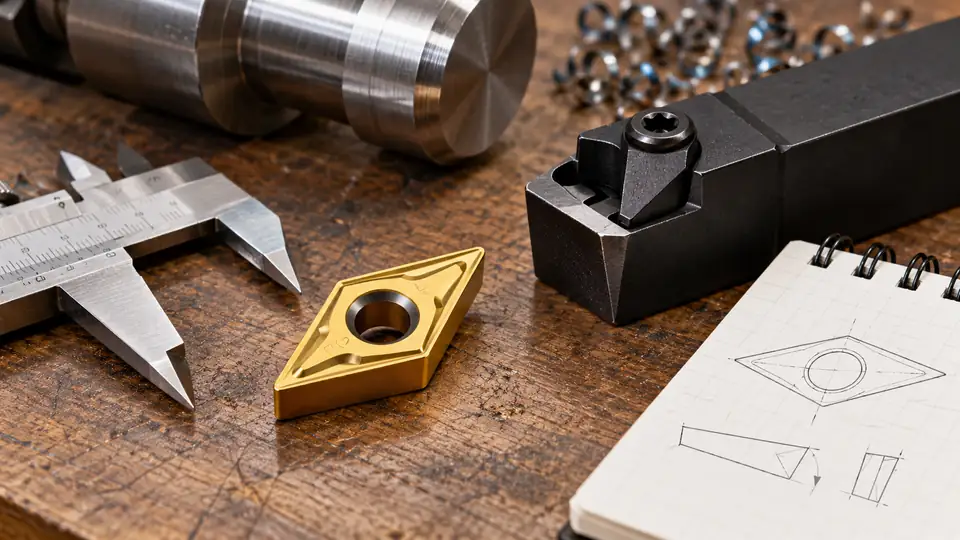
Carbide insert codes describe an insert’s standardized geometry and dimensions. A designation such as CNMG 120408 identifies the shape, clearance angle, tolerance class, physical configuration, size, thickness, and corner radius. It does not normally identify the carbide grade, coating, chipbreaker geometry, or exact toolholder compatibility without additional catalog information.
Most indexable turning inserts use a designation based on ISO 1832. U.S. catalogs may also show an ANSI inch-style dimensional code. Reading the letter portion first, then identifying the dimensional system, prevents many compatibility errors.
Once you have the full designation, our guide to carbide turning inserts for your holder helps compare the geometry, grade, and intended material.
How an Insert Designation Is Structured
A typical ISO metric designation can be separated as follows:
CNMG 120408
- C: insert shape
- N: clearance angle
- M: tolerance class
- G: insert configuration
- 12: standardized size designation
- 04: thickness designation
- 08: corner-radius designation
The first four characters describe geometry and construction. The following characters describe nominal dimensions through the applicable coding system. Manufacturer-specific suffixes commonly follow the standardized designation.
| Position | What It Describes | Example From CNMG 120408 |
|---|---|---|
| 1 | Insert shape | C, 80-degree diamond |
| 2 | Normal clearance angle | N, 0 degrees |
| 3 | Tolerance class | M |
| 4 | Configuration, including standardized hole and surface features | G |
| 5 | Size designation | 12 |
| 6 | Thickness designation | 04 |
| 7 | Corner-radius designation | 08 |
Optional characters may communicate cutting-edge condition, cutting direction, or other standardized details. Catalog suffixes can then specify a chipbreaker and carbide grade. Their position and format vary among manufacturers.
First Letter: Insert Shape
The first letter identifies the insert’s outline when viewed from above. Shape affects cutting-edge strength, profiling access, approach geometry, and the holder pocket required to support the insert.
| Code | Basic Shape | Included Corner Angle | Common Characteristic |
|---|---|---|---|
| C | Diamond | 80 degrees | Relatively strong corner for general turning |
| D | Diamond | 55 degrees | Greater profiling access than an 80-degree insert |
| R | Round | Not applicable | Strong continuous edge, with contact geometry that changes by depth of cut |
| S | Square | 90 degrees | Strong corners where holder and workpiece clearance permit |
| T | Triangle | 60 degrees | Multiple indexed corners and moderate profiling access |
| V | Diamond | 35 degrees | Good access for detailed profiling, with a less-supported corner |
| W | Trigon | 80 degrees | Three-lobed form providing several usable corners |
Two inserts with different shape letters cannot be treated as substitutes. A C-shaped insert and a D-shaped insert require different pocket geometry, despite both being described as diamond-shaped.
Second Letter: Clearance Angle
The second character gives the insert’s normal clearance, also called the relief angle. This is the angle between the flank below the cutting edge and a line perpendicular to the insert’s seating surface.
| Code | Normal Clearance Angle |
|---|---|
| N | 0 degrees |
| A | 3 degrees |
| B | 5 degrees |
| C | 7 degrees |
| P | 11 degrees |
| D | 15 degrees |
| E | 20 degrees |
| F | 25 degrees |
| G | 30 degrees |
An N insert has zero normal clearance and is commonly described as a negative insert. Many such turning inserts can provide usable edges on both faces, provided their complete geometry and clamping configuration support double-sided indexing.
A C insert has 7 degrees of relief and is commonly called positive. Positive-clearance inserts are generally single-sided because the relief is formed into the insert body. The insert’s effective cutting geometry still depends on the holder’s seat and orientation.
Third Letter: Tolerance Class
The third character identifies a dimensional tolerance class. Depending on the insert shape and standard, the class controls allowable variation in features such as the inscribed circle, thickness, and cutting-point position.
M is common on molded and sintered general-purpose turning inserts. G is commonly associated with more closely controlled, often ground inserts. That distinction does not mean every G-class insert is preferable to every M-class insert. Precision, edge preparation, grade, chipbreaker, and application must be evaluated together.
Tolerance letters should not be converted into one universal plus-or-minus value. The applicable limits depend on insert size, shape, measured feature, and standard table.
Fourth Letter: Insert Configuration
The fourth character describes the standardized insert type or configuration. It can account for combinations of features such as:
- A central mounting hole
- A cylindrical or countersunk hole
- Single-sided or double-sided countersinking
- Chip-control features on one or both faces
- The relationship between the hole and insert faces
For example, the fourth characters in CCMT, CNMG, and VBMT are T, G, and T respectively. These letters must be interpreted through the relevant standard or the manufacturer’s dimensional drawing. Treating the fourth character as a simple chipbreaker code can produce the wrong insert.
A chipbreaker often appears as a separate suffix, such as a manufacturer’s two-letter or alphanumeric designation. Such suffixes are generally proprietary and cannot be decoded reliably through the ISO geometry table.
Reading the Dimensional Characters
The characters following the first four letters identify size, thickness, and corner radius. Their interpretation depends on whether the catalog uses an ISO metric code or an ANSI inch-style convention.
ISO Metric-Style Codes
In a designation such as CNMG 120408:
- 12 is the standardized size code.
- 04 is the thickness code.
- 08 represents a nominal 0.8 mm corner radius.
A common CNMG 120408 insert has a nominal 12.7 mm inscribed circle, a nominal 4.76 mm thickness, and a 0.8 mm corner radius. The size and thickness codes should still be checked against a dimensional table. They are designation fields rather than instructions to insert a decimal point.
Some metric thickness positions use a letter. For example, CCMT 09T304 commonly describes an insert with a nominal 9.525 mm inscribed circle, 3.97 mm thickness, and 0.4 mm corner radius. Here, T3 is the thickness designation. It should be read as a coded field, not as the literal measurement “T3 millimeters.”
ANSI Inch-Style Codes
U.S. catalogs may list the same general insert dimensions with an inch-style code. For many common turning inserts, the dimensional fields are based on fractional inches:
- The size digit commonly represents eighths of an inch.
- The thickness field commonly represents sixteenths of an inch.
- The nose-radius digit commonly represents sixty-fourths of an inch.
For example, CNMG 432 is commonly interpreted as:
- 4: 4/8 inch, or 1/2-inch nominal inscribed circle
- 3: 3/16-inch nominal thickness
- 2: 2/64 inch, or 1/32-inch nominal corner radius
Those values correspond approximately to 12.7 mm, 4.76 mm, and 0.8 mm, which aligns with CNMG 120408. Fractional thickness designations can include additional digits or decimal-style notation, so the catalog’s coding table remains necessary.
Common Insert Families at a Glance
The following families illustrate how the first characters change geometry. They are separate insert types, not interchangeable variations of one insert.
| Family | Shape | Clearance | Tolerance | Configuration Code |
|---|---|---|---|---|
| CCMT | 80-degree diamond | 7 degrees | M | T |
| CNMG | 80-degree diamond | 0 degrees | M | G |
| DCMT | 55-degree diamond | 7 degrees | M | T |
| WNMG | 80-degree trigon | 0 degrees | M | G |
| TNMG | 60-degree triangle | 0 degrees | M | G |
| VBMT | 35-degree diamond | 5 degrees | M | T |
CCMT and CNMG begin with the same shape letter, but their clearance angles and configurations differ. DCMT offers a more acute 55-degree corner. VBMT uses a still narrower 35-degree point. Those changes affect holder design, edge support, workpiece access, and suitable operations.
Codes That the Standardized Geometry Does Not Explain
A complete catalog description may look more complex than the basic designation because manufacturers append their own identifiers. These commonly cover three areas.
Chipbreaker
The chipbreaker describes molded or ground features near the cutting edge that influence chip formation and cutting behavior. A code such as PM, MF, or another suffix has no dependable cross-brand meaning. One manufacturer’s PM geometry may differ substantially from another manufacturer’s identically lettered geometry.
For stainless-steel work, compare carbide inserts for stainless-steel turning by chipbreaker, grade, and the exact holder seat.
Carbide Grade and Coating
Grade codes identify the cutting material selected by the manufacturer. The grade may differ in carbide composition, binder, grain structure, coating system, edge preparation, and intended workpiece range.
A grade number is usually proprietary. It cannot be decoded as insert size or assumed to match another brand’s grade with a similar number. The base designation may also be used for ceramic, CBN, PCD, or other cutting materials, so a geometry code alone does not prove that the insert is cemented carbide.
For nonferrous turning, compare carbide inserts for aluminum by grade and edge geometry as well as the code.
Edge Preparation and Hand
Additional characters may identify a honed, chamfered, sharp, or specially prepared edge. Some designations also identify right-hand, left-hand, or neutral cutting direction. These details matter in specialized operations, but their presentation differs across catalog systems.
How to Match an Insert to a Toolholder
Visual similarity is insufficient for confirming compatibility. Use the holder manufacturer’s documentation and compare the complete insert specification.
- Read the holder marking. Record the full holder designation and any stated insert family.
- Match the first four insert characters. Shape, clearance, tolerance, and configuration must agree with the pocket and clamping system.
- Verify size and thickness. An insert with the same letters can still have a different inscribed circle, cutting-edge length, or thickness.
- Check the corner radius. The holder may physically accept several radii, but radius changes influence clearance, programmed tool-nose compensation, cutting forces, and finish.
- Confirm the mounting features. Hole diameter, countersink, clamp style, seat, shim, and screw must match the holder specification.
- Select the chipbreaker and grade separately. Base this selection on the workpiece material, operation, cutting conditions, setup rigidity, and manufacturer guidance.
Do not force an insert into a pocket or substitute a different clamp screw. Carbide inserts can fracture if they are poorly seated, over-tightened, unsupported, or used with damaged clamping components. Clean the pocket and inspect the seat, screw, clamp, and shim before installation. Follow the holder manufacturer’s torque and assembly instructions.
On a small lathe, choose mini-lathe replacement inserts only after matching the holder’s full insert designation.
Frequent Decoding Errors
- Reading every number as millimeters. Metric designation fields are coded positions, and inch-style codes use fractional conventions.
- Ignoring the dimensional system. CNMG 120408 and CNMG 432 can describe corresponding nominal dimensions through different systems.
- Treating M as a material code. In the third position, M identifies a tolerance class. It does not mean medium machining or a particular carbide grade.
- Calling the fourth letter a chipbreaker. That position identifies standardized configuration. Proprietary chipbreaker codes usually appear separately.
- Assuming a geometry code means carbide. The same standardized shape may be manufactured from several cutting-tool materials.
- Matching by the first four letters alone. Size, thickness, radius, mounting details, and holder requirements still have to agree.
- Assuming suffixes work across brands. Grade and chipbreaker codes generally require the issuing manufacturer’s catalog.
A Reliable Way to Read Any Insert Code
Start by separating the designation into standardized geometry, standardized dimensions, and proprietary suffixes. Decode the first four letters through ISO 1832 terminology. Determine whether the dimensional section uses a metric or inch-style system, then confirm the actual measurements from a dimensional drawing.
Finally, treat chipbreaker and grade identifiers as manufacturer-specific information. A fully matching insert must have the required geometry, dimensions, mounting configuration, and application characteristics. Shared shape letters or a close visual resemblance do not establish toolholder compatibility.
